High-precision commercial kitchen units manufactured to stringent international quality and safety benchmarks.
Analyzing thermal preservation dynamics, strict HACCP compliance, and next-generation holding cabinet technologies across international hospitality networks.
The global commercial food warming and thermal preservation equipment market has underwent a major technological evolution. No longer treated as simple passive heat cabinets, modern commercial food warmers, countertop heated display cases, and insulated holding cabinets serve as crucial nodes in food safety governance, operational workflow optimization, and sensory quality retention for multinational restaurant chains, luxury hotel groups, and high-volume catering enterprises.
Driven by rigid international regulatory benchmarks—such as NSF/ANSI Standard 4 for hot holding equipment, CE directives, UL safety mandates, and global Hazard Analysis Critical Control Point (HACCP) frameworks—the demand for precision-engineered food holding apparatus has accelerated worldwide. Commercial kitchens require systems capable of holding cooked food at core temperatures strictly above 60°C (140°F) to prevent pathogen propagation while simultaneously managing micro-humidity environments to prevent product degradation, soggy crusts, or thermal drying.
Information Gain Insight: Advanced heat-transfer modeling demonstrates that precise radiant heating combined with controlled moisture injection reduces energy consumption by up to 28% compared to traditional open water-pan Bain-Maries, while extending organoleptic food quality holding times by an average of 45%.
As global ghost kitchens (cloud kitchens), Quick Service Restaurant (QSR) chains, and hotel banqueting setups expand, sourcing partners prioritize energy efficiency, modular stackability, smart connectivity, and durable AISI 304 stainless steel construction. Chinese manufacturing hubs, spearheaded by industrial strongholds such as Guangzhou, have emerged as the premier global supply ecosystem for high-spec, cost-effective, and fully customizable thermal holding solutions.
High-density polyurethane insulation paired with smart micro-pulse heating elements drastically minimizes thermal leakage and operational electricity costs.
Automated micro-controller temperature tracking prevents microbial growth within the critical food safety zone (4°C to 60°C / 40°F to 140°F).
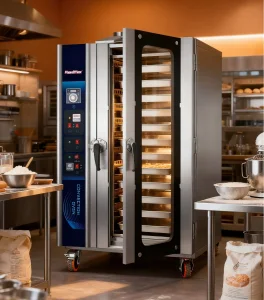
Designed to standard Gastronorm (GN 1/1, GN 2/1) dimensions, facilitating seamless cross-equipment compatibility with combi steam ovens and prep stations.
Discover how structural industrial synergies, advanced metallurgy, and scale economies position Guangzhou suppliers at the pinnacle of global export efficiency.
China’s commercial catering equipment industry has transitioned from high-volume assembly to advanced engineering, proprietary automated manufacturing, and high-end OEM/ODM customized output. Procurement officers from North America, Europe, the Middle East, and Southeast Asia increasingly partner with Chinese manufacturers to achieve superior cost-to-performance ratios without sacrificing structural integrity.
The Pearl River Delta economic zone—centered around Guangzhou—represents the world's most concentrated ecosystem for commercial food prep, baking, and thermal holding appliances. This cluster offers unparalleled structural advantages:
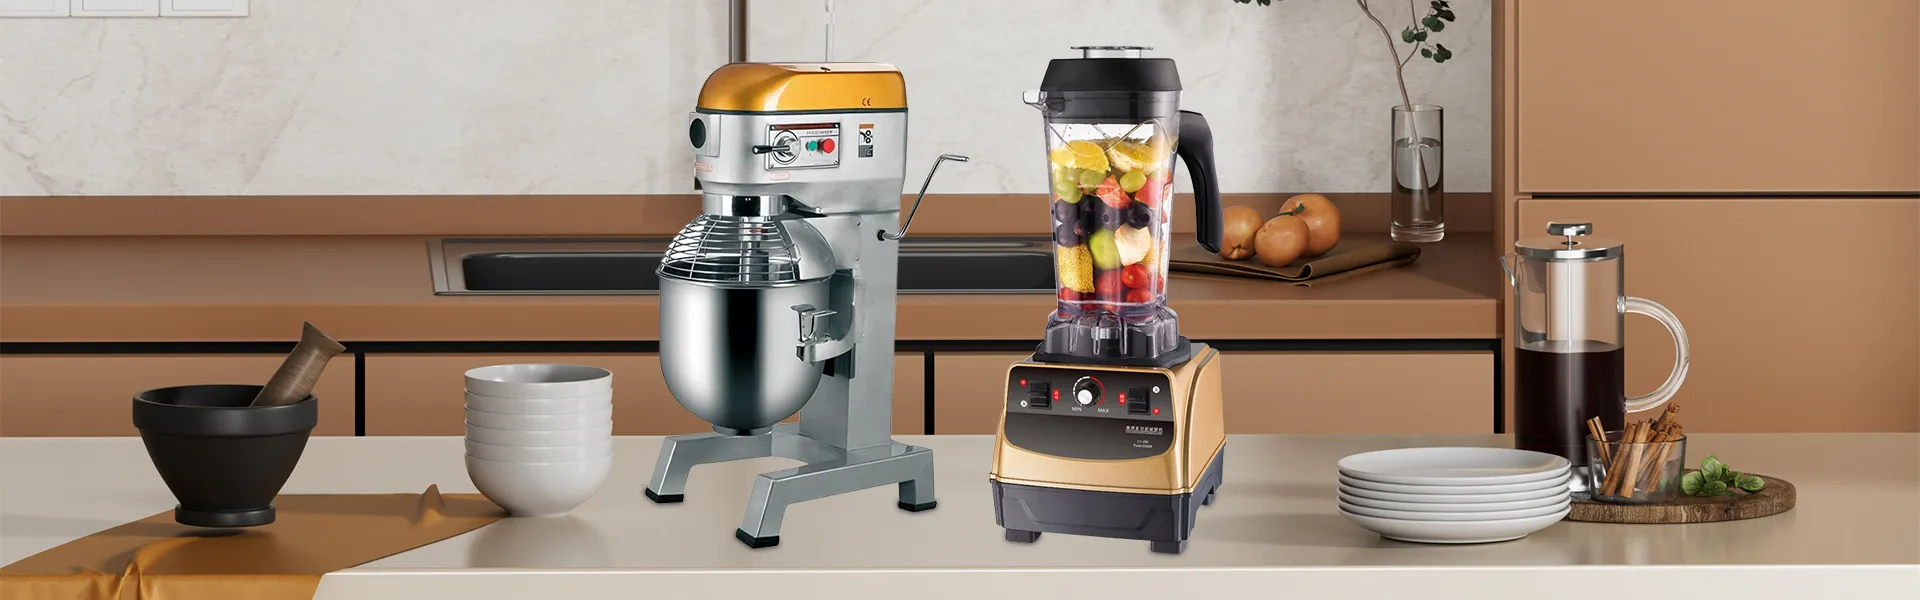
A premier Chinese enterprise delivering world-class commercial food warmers, bakery machines, and complete commercial kitchen systems.
Guangzhou Chef Nest Kitchen Co., Ltd. is a professional manufacturer and supplier specializing in high-quality kitchen appliances and commercial cooking solutions. Located in Guangzhou, Guangdong Province, one of China’s leading industrial and trade hubs, the company benefits from a strategic location with convenient access to domestic and international markets. Covering an area of over 10,000 square meters, Chef Nest Kitchen operates modern production facilities equipped with advanced assembly lines, quality inspection laboratories, and efficient logistics systems. The company focuses on designing and producing innovative, durable, and user-friendly kitchen products that meet the diverse needs of restaurants, hotels, catering services, and households worldwide.
Since its establishment, Guangzhou Chef Nest Kitchen has grown steadily, expanding both its product portfolio and market reach. The company’s offerings include commercial ovens, electric cooking appliances, food processors, beverage machines, and other kitchen equipment designed for efficiency and safety. Over the past decade, Chef Nest Kitchen has invested in research and development, enabling it to launch a series of products that combine smart functionality, energy efficiency, and ergonomic design. With a strong emphasis on quality management, the company ensures that every product undergoes rigorous testing before leaving the factory.
Guangzhou Chef Nest Kitchen employs over 150 skilled professionals, including engineers, technical specialists, quality inspectors, and sales personnel. This team is dedicated to providing exceptional customer service and technical support to clients worldwide. Guided by principles of innovation, reliability, and customer satisfaction, Guangzhou Chef Nest Kitchen Co., Ltd. continues to expand its global footprint, offering trusted kitchen solutions and building long-term partnerships with distributors, restaurants, and catering enterprises in multiple regions.
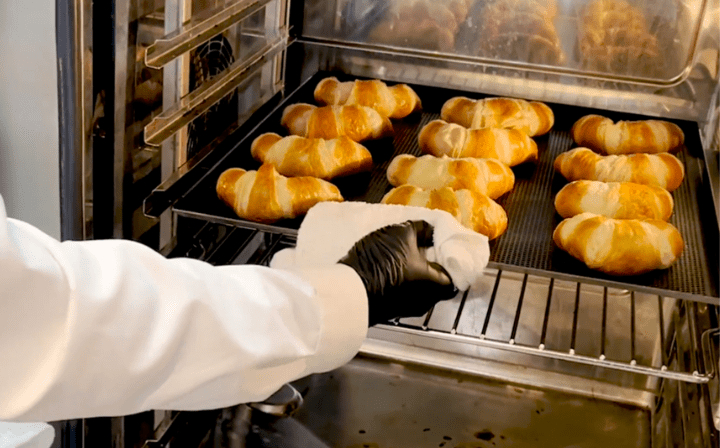
Engineered for versatile deployment across diverse commercial food service workflows and severe high-duty industrial environments.
Under-counter waterless holding drop-ins and decorative countertop heated displays maintain delicate proteins, sauces, and seafood at exact serving temperatures without altering texture.
Pass-through holding cabinets allow kitchen staff to load cooked burgers, fries, and fried chicken from the rear while front-of-house staff dish out orders without thermal loss.
Proofer-warmer dual cabinets combine precise micro-humidity proofing for raw dough with warming capabilities for baked goods like pies, croissants, and artisan breads.
Heavy-duty mobile banqueting carts with insulated rubber bumpers transport hundreds of pre-plated meals across hospital wings or campus dining halls while maintaining strict heat retention.
Smart multi-compartment warming lockers keep completed delivery orders at safe hold temperatures until delivery drivers authenticate pickup via digital passcode.
Specialized marine-grade food warmers featuring flanged feet, anti-spill retaining latches, and heavy 316-grade stainless steel to resist salt-corrosion in cruise ships and offshore platforms.
How AI-driven sensor technology, precision humidity control, and advanced thermodynamics redefine food warming efficiency.
Proportional-Integral-Derivative (PID) controllers actively continuously sense cavity temperatures, making micro-adjustments every millisecond to eliminate thermal overshoot and maintain internal variance under ±0.5°C.
Active water atomization systems automatically balance relative humidity levels (RH 10% to 90%), retaining food crispness or moisture without oversaturating or drying delicate items.
Built-in Wi-Fi and Bluetooth modules continuously transmit thermal logs to cloud dashboards, generating compliance reports for health inspectors and alerting staff to door breaches.
Use this comparative matrix to evaluate heating technologies when selecting commercial food warming and holding equipment.
| Heating Technology | Temperature Range | Humidity Control | Best Product Application | Energy Efficiency |
|---|---|---|---|---|
| Convection Air Heating | 30°C - 90°C (86°F - 194°F) | Low / Dry Ambient | Fried chicken, french fries, baked pies, crispy snacks | High (Fast Recovery) |
| Halo Heat / Soft Radiant | 30°C - 95°C (86°F - 203°F) | Passive Natural Moisture Retention | Roast beef, ribs, poultry, sensitive proteins | Ultra-High (Low Wattage) |
| Water-Pan Humidity Bain Marie | 40°C - 85°C (104°F - 185°F) | High Continuous Vapor | Soups, stews, gravies, steamed rice, cooked vegetables | Medium |
| Infrared Quartz Lamp Warmers | Surface Radiant Heat | None (Open Counter) | Plated meals ready for pickup, pass-through service lines | Targeted Spot Heating |
Expert answers regarding food warming compliance, manufacturing standards, and international sourcing dynamics.
According to international FDA and HACCP standards, hot food must be maintained at an internal core temperature of 60°C (140°F) or higher. Keeping hot holding units set between 65°C and 75°C ensures bacteria cannot multiply while preserving eating quality.
Key certifications include CE (for European electrical and safety compliance), ETL / UL (for North American safety standards), NSF/ANSI 4 (for commercial sanitation compliance), and ISO9001 factory quality management certification.
Dry warmers rely solely on radiant or forced air heat, making them ideal for crispy foods like fried chicken or pastries. Humidified cabinets inject controlled moisture, making them optimal for meats, cooked vegetables, and sauces that dry out easily.
Yes. Guangzhou Chef Nest Kitchen Co., Ltd. provides full OEM/ODM services, including customized stainless steel dimensions, specialized voltage configurations (110V/220V/380V, 50Hz/60Hz), custom control interfaces, and private logo branding.
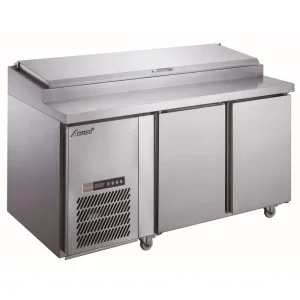
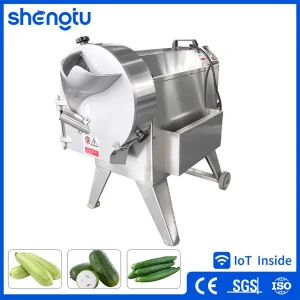
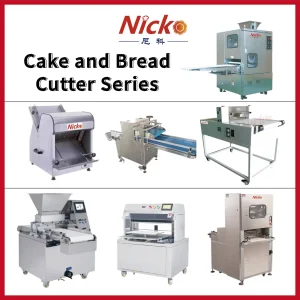
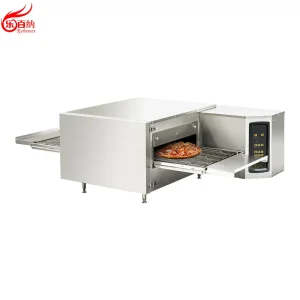
Explore our full range of heavy-duty industrial kitchen machinery designed for long operational lifespans.
 Chef Nest Kitchen