Food processing quality is the quiet promise behind every carton, pouch, and frozen shipment. Global buyers expect safe products, consistent specifications, and evidence that both are controlled. A clean factory helps, but appearance alone proves very little. Quality is built through disciplined routines, verified measurements, and responsible decisions when conditions change.
In practice, teams should examine what factors affect food processing quality at every production stage. Raw material freshness, supplier performance, water quality, equipment hygiene, processing temperatures, and employee training can alter the final product. For example, a two-degree temperature drift may affect texture or microbial control. A delayed delivery can also weaken an otherwise stable production plan. Clear batch records, calibrated instruments, and traceability exercises help buyers follow each lot from origin to shipment. These details matter during audits and during unexpected complaints.
No facility is flawless. That deserves honest attention. Cleaning logs may be complete, while actual cleaning remains inconsistent. Training may be documented, while temporary workers still misunderstand allergen controls. Audits are useful, but they capture limited moments. Reliable processors therefore review data continuously, investigate deviations, and improve procedures without hiding inconvenient results. Independent laboratory testing and recognized food safety systems can strengthen confidence, but certificates cannot replace daily discipline. Buyers should see practical evidence: labeled containers, separated allergen tools, cold rooms with visible temperature records, and staff who can explain their checks clearly. Quality becomes credible when the process remains controlled, transparent, and repeatable across borders.
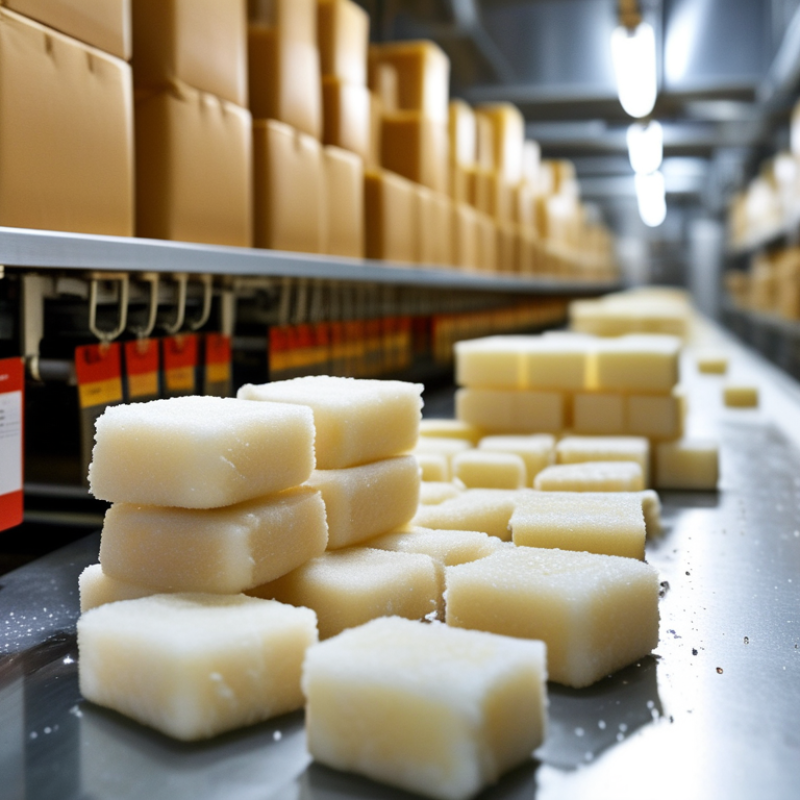
Global food processing quality begins with a written definition of requirements. Buyers need more than a general promise of safety. They need measurable limits for moisture, acidity, temperature, weight, texture, and shelf life. Each product specification should identify approved ingredients, allergen controls, packaging materials, and storage conditions. Clear limits reduce disputes before production starts.
Experienced processors also define how quality will be checked. A practical plan may include calibrated thermometers, batch sampling, sanitation records, and laboratory testing. Test methods must be suitable for the product and accepted by the buyer’s market. Traceability should connect each finished carton to raw materials, operators, equipment, and production time. During supplier discussions, request written acceptance criteria, inspection frequency, and procedures for handling rejected batches. Small details matter.
Global requirements are not always identical. Temperature expectations, labeling information, documentation, and cultural preferences can vary between markets. An experienced quality team reviews destination requirements with qualified advisers and keeps controlled records of updates. Do not rely on old templates. They become inaccurate. In my experience, teams often measure what is easy rather than what creates risk. That weakness deserves honest review.
Global buyers expect more than attractive packaging. They need safe ingredients, controlled equipment, and repeatable production methods. Ingredient approval should begin with a documented specification. Check origin, allergen status, shelf life, and contamination risks. Request current certificates and test results from qualified suppliers. Review them carefully. A certificate alone does not prove every batch is suitable.
Equipment must support hygienic design and reliable cleaning. Product-contact surfaces should resist corrosion and avoid hidden gaps. Temperature sensors, scales, and metal detectors require scheduled calibration. Keep calibration records available for buyer audits. Production areas also need controlled water quality, airflow, pest prevention, and employee hygiene. A polished factory can still contain weak control points.
Production methods should follow a written food safety plan, such as HACCP-based procedures. Define critical limits for heating, cooling, filling, and storage. Record real measurements, not estimates. Traceability should connect finished cartons to ingredients, operators, and processing times. Test the recall process before a buyer requests it. It may reveal missing codes or slow communication. This is where many systems fail. Corrective actions should identify the cause, not only repair the visible defect. Buyer specifications can also differ by destination, so review labeling, testing, and documentation requirements for each market. Perfect control is unlikely, but honest records and disciplined improvement build dependable quality.
Global buyers do not inspect intentions; they inspect repeatable controls. A standardized hygiene system starts with defined zones, not a generic cleaning checklist. Separate raw and ready-to-eat routes physically. Mark doors, tools, drains, and handwashing points. Keep it visible. The WHO report Foodborne Disease Burden Epidemiology Reference Group estimates that contaminated food causes 600 million illnesses and 420,000 deaths annually. That risk makes documented prevention a commercial requirement.
Every critical step needs an owner, limit, record, and response. For example, operators can record product temperatures at receiving, cooking, cooling, and dispatch. Calibrate probes on a fixed schedule. An ATP swab can support verification, but it cannot replace microbiological testing. The USDA Economic Research Service estimated the annual cost of foodborne illness in the United States at 15.5 billion dollars, using data published in its 2015 report. These figures are not identical across countries, but they show why buyers examine process evidence, not appearance.
Traceability should reach the ingredient lot, production line, shift, and shipment. Test mock recalls regularly. A two-hour exercise can expose missing records, unclear responsibilities, and weak communication. Suppliers should also review sanitation chemicals, allergen changeovers, pest findings, and employee training. In practice, records are often completed after production. That weakness matters. A missed signature should trigger investigation, not silent correction. Internal audits should include floor observations and worker interviews. No system is perfect. Teams sometimes chase paperwork while overlooking a leaking seal or a blocked drain. Buyers trust suppliers that detect these gaps and document the corrective action.
Food processing quality begins with evidence, not attractive packaging.
The World Health Organization estimates that contaminated food causes 600 million illnesses and 420,000 deaths each year.
These figures come from its Global Burden of Foodborne Diseases report. They show why global buyers request more than a supplier declaration.
Testing should match the product’s risks.
A laboratory accredited to ISO/IEC 17025 can examine pathogens, allergens, residues, moisture, and heavy metals.
Samples need clear lot numbers, collection times, temperatures, and chain-of-custody records.
Keep retention samples from every production batch.
A simple barcode can connect raw materials, processing equipment, test results, and shipping documents.
When a result fails, traceability should identify affected cartons within hours, not days.
The U.S. Food and Drug Administration’s New Era of Smarter Food Safety blueprint also emphasizes stronger traceability and digital records.
Digital systems help, but they do not replace trained workers. Someone must verify the label, seal, and sample condition.
Errors still happen.
A rushed sample can weaken a reliable test. An incomplete supplier record can delay a recall.
That uncomfortable gap deserves regular review.
Internal audits should challenge assumptions, while corrective actions should include deadlines and responsible staff.
Buyers may trust a transparent explanation more than a flawless-looking file.
Test consistently. Record honestly.
How to Ensure Food Processing Quality for Global Buyers?
Reliable food quality begins with evidence, not promises. Processing teams should prepare for audits every day, not only before a buyer’s visit. Keep approved specifications, allergen controls, sanitation checks, and temperature logs in one controlled system. Each record should show who completed it, when it was checked, and what happened after a deviation. Clear lot codes also help teams trace ingredients from receiving to shipment within minutes.
Small details matter. A wet signature, unclear correction, or missing calibration record can weaken buyer confidence. Auditors often inspect cold-room readings, cleaning schedules, pest-control reports, and employee training files. Records must be accurate and easy to retrieve. Never rewrite history. Correct errors transparently, explain the cause, and document the approved action.
Tips: Run short mock audits each month. Select one lot and trace it backward and forward. Interview operators near the production line. Check whether written procedures match real behavior. Review corrective actions for repeated problems, not just closed forms. Continuous improvement requires honest reflection. No system is flawless. A team may discover that a checklist is completed too quickly or that a measuring device is rarely verified. Treat these findings as useful signals. Update procedures, retrain staff, and measure whether the change works. Global buyers value consistent results, clear communication, and proof that improvements remain effective.
Reference-based food safety and quality control dashboard for export-oriented processing operations
| Control Area | Quality Dimension | Reference-Based Requirement or KPI | Required Records and Evidence | Review Frequency | Suggested Performance Target |
|---|---|---|---|---|---|
| Food Safety System | Hazard analysis and preventive controls | Apply the seven HACCP principles: hazard analysis, CCP identification, critical limits, monitoring, corrective action, verification, and recordkeeping. | Approved hazard analysis, process flow diagram, CCP decision records, validation and verification reports. | At least annually and whenever products, processes, equipment, or regulations change. | 100% of identified hazards controlled |
| Critical Control Points | Monitoring compliance | Each critical limit must be measurable, monitored at defined intervals, and linked to documented corrective action. | Temperature logs, time records, metal detector checks, corrective-action reports, supervisor sign-offs. | Every production batch or defined monitoring interval. | ≥99.5% complete monitoring records |
| Supplier Approval | Incoming material conformity | Use risk-based supplier approval, specifications, receiving checks, and periodic performance evaluation. | Supplier questionnaire, certificates, specifications, certificates of analysis, receiving inspection records. | Each delivery; supplier reassessment at least annually or according to risk. | 100% approved suppliers before purchasing |
| Allergen Management | Cross-contact prevention and labeling | Identify allergens in ingredients and products, control cross-contact, and verify label accuracy before release. | Allergen matrix, line-clearance checklist, cleaning validation, label approval and verification records. | Every product changeover and every label revision. | Zero mislabeled allergen incidents |
| Traceability | One-step-back and one-step-forward tracking | Maintain records showing the immediate supplier and the immediate business customer for each relevant lot, consistent with international traceability principles. | Lot codes, receiving records, production records, dispatch records, customer distribution lists. | Each lot; system test at least annually. | 100% lot linkage; mock trace completed within 4 hours |
| Record Control | Accuracy, integrity, and retention | Records should be legible, protected from unauthorized changes, readily retrievable, and retained for the applicable legal or customer-defined period. U.S. preventive-control records are generally retained for at least two years. | Controlled forms, electronic audit trails, retention schedule, access-control logs, document revision history. | Routine review monthly; formal document review at least annually. | ≥98% records retrievable within one business day |
| Calibration | Measurement reliability | Food safety measurement devices must be calibrated or verified against recognized standards at defined intervals and after damage or suspected inaccuracy. | Calibration certificates, verification checks, equipment register, out-of-tolerance assessment. | According to risk and manufacturer guidance; commonly every 6–12 months. | 100% critical devices within calibration date |
| Internal Audits | System conformity and effectiveness | Use a documented, risk-based audit program covering food safety, quality, legal, customer, sanitation, and process requirements. | Audit schedule, auditor competence records, findings, root-cause analysis, corrective-action verification. | High-risk processes quarterly; full system at least annually. | 100% planned audits completed on schedule |
| Corrective Action | Root-cause resolution | Contain affected product, investigate the root cause, implement corrective action, and verify that recurrence has been prevented. | Nonconformance report, containment evidence, root-cause analysis, action owner, effectiveness check. | Immediate containment; action review weekly until closure. | ≥95% actions closed by agreed due date |
| Product Release | Batch conformity | Release only after required process records, test results, packaging checks, and label verification meet approved specifications. | Batch release checklist, laboratory results, packaging inspection, deviation approval. | Every batch or shipment. | 100% batches released by authorized personnel |
| Continuous Improvement | Trend analysis and management review | Analyze complaints, deviations, audit findings, laboratory results, waste, and supplier performance to prioritize measurable improvement actions. | KPI dashboard, complaint trend report, management-review minutes, improvement project records. | Monthly KPI review; formal management review at least annually. | Year-on-year reduction in repeat nonconformities |
: It should define limits for moisture, acidity, temperature, weight, texture, and shelf life. It should also list approved ingredients, allergens, packaging, and storage conditions. Vague promises create disputes.
Separate raw and ready-to-eat areas with marked doors, tools, drains, and handwashing points. Assign an owner, limit, record, and response to every critical step. Keep it visible.
Record temperatures during receiving, cooking, cooling, and dispatch. Use calibrated probes and follow a fixed checking schedule. A missed reading needs investigation, not silent completion.
Traceability should connect each carton with ingredients, equipment, operators, shifts, test results, and shipment details. Simple barcodes can reduce searching time. Records must work under pressure.
Testing should reflect product risks, including pathogens, allergens, residues, moisture, or heavy metals. Use qualified laboratories and clear sample records. Record lot numbers, collection times, temperatures, and custody details.
Identify affected cartons quickly and place them on hold. Investigate the cause, assign corrective actions, and set completion deadlines. Do not hide the original deviation.
A realistic recall exercise can reveal missing records, unclear duties, and weak communication. A two-hour exercise may expose problems before a real incident. Some gaps feel embarrassing.
Audits should include floor observations, worker interviews, sanitation checks, and equipment inspections. Look for leaking seals, blocked drains, missed signatures, and late records. Paperwork can create false confidence.
Ensuring food processing quality for global buyers requires a clear, systematic approach from sourcing to delivery. Companies should first define the quality, safety, labeling, and documentation requirements of each target market. Understanding what factors affect food processing quality, including ingredient condition, equipment performance, production methods, hygiene, temperature control, and staff practices, helps establish effective preventive measures. Selecting compliant ingredients, well-maintained equipment, and suitable processing techniques is essential for producing consistent and safe products.
A standardized hygiene and process control system should cover cleaning, sanitation, personnel training, critical control points, and contamination prevention. Product safety must be verified through appropriate testing, batch identification, and traceability records that support rapid investigation when necessary. Regular internal reviews, customer audits, accurate documentation, and corrective actions help maintain compliance over time. By monitoring performance, learning from deviations, and continuously improving processes, food processors can build buyer confidence, reduce quality risks, and deliver reliable products across international markets.
Chef Nest Kitchen